To view the technical documents, please fill out the form below. We will get back to you as soon as possible and you can log in and review with the password given by us. If you have a password, you can log in and continue by clicking "Sign In".
You can access the documentation by logging in from this area with the password given to you.
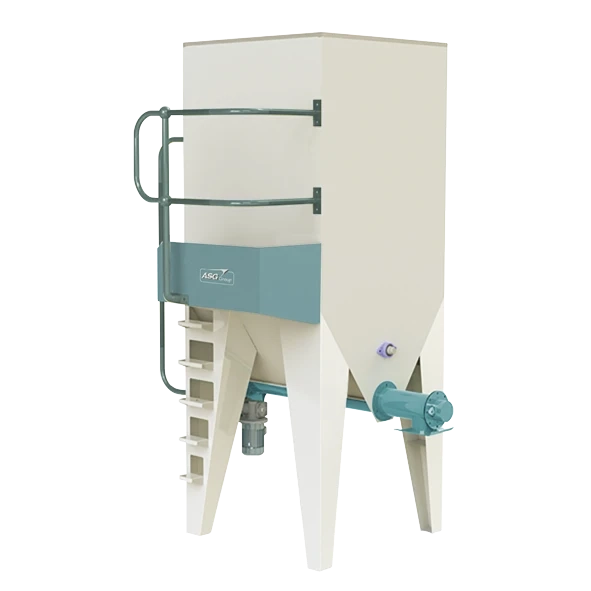
Volumetric raw-material distribution unit with integrated mixer and inverter control
A high-capacity discharge and precise-dosing unit for plants that store their raw materials in big-bag packaging during logistics and storage — above all in the food, chemical, plastics and feed industries. While ensuring the OHS-compliant, fast and loss-free discharge of large-volume big-bags, it is, with the mechanics in its lower body, a multi-purpose operation centre that transfers the collected product to the next process in a controlled way and in the desired proportions.
WORKING PRINCIPLE
Safe big-bag suspension and discharge management — ergonomic package discharge: the big-bag package suspended on the carrier chassis by crane or forklift is safely positioned over the hopper’s upper intake mouth; when the package lock is opened, the bulk raw material passes by gravity into the dust-tight rigid hopper body. Inner-mixer activation and bridging prevention — forced fluidisation: the heavy-duty mechanical mixer (agitator) integrated into the hopper body engages; this mechanism reliably prevents the shed dust or granular raw material from compacting, clumping in the chamber or sticking to the walls and bridging — it guarantees a continuous flow. Speed-control-regulated uniform injection — inverter-controlled precise conveying: the drive unit connected to the hopper’s outlet line is commanded by a smart speed-control device (inverter / frequency converter); the system feeds the raw material in precise proportions set from the control room or to the next machine with full uniform stability.
KEY ADVANTAGES
- Multi-purpose modular structure and wide application range: Designed with a flexible engineering design to fully suit general-purpose industrial uses; by successfully collecting in a single chamber the products of various characters arriving from different points, it provides in-plant logistic synchronisation.
- Uninterrupted product flow via the mechanical mixer: It breaks the gravity-flow resistance of dense or static-prone dust materials with a low flowability index by the continuously rotating mixer-blade system inside the body; it creates a stable, clog-free material bed.
- Flexible recipe management via the speed-control device: The speed of the outlet transfer mechanism can be precisely set through the automation; this infrastructure allows the raw-material injection to be precisely metered according to the plant’s instantaneous production output or the target grist recipes.
- Ergonomic viewing platform and integrated ladder: Because of the construction’s high vertical form, a protected access ladder fully compliant with occupational-health-and-safety (OHS) rules is included in the system; the balcony-shaped projection (viewing platform) at the body edge lets the operator comfortably monitor the internal mechanical state and the product flow.
ENGINEERING NOTE
Big-bag discharge and dosing hoppers are a critical pre-process component of bulk-raw-material reception stations, simultaneously raising labour productivity and minimising dust emissions. The body volume’s static-strength calculations are verified by computer-aided analysis (FEA) so as to damp the impact loads the big-bag creates during instant discharge. The inner-mixer paddle geometry, combined with the optional frequency-converter screw/injector-airlock discharge, guarantees the raw material is fed to the lower lines uniformly, in the form of a flour curtain, without clogging.
 TR
 RU
 ES