To view the technical documents, please fill out the form below. We will get back to you as soon as possible and you can log in and review with the password given by us. If you have a password, you can log in and continue by clicking "Sign In".
You can access the documentation by logging in from this area with the password given to you.
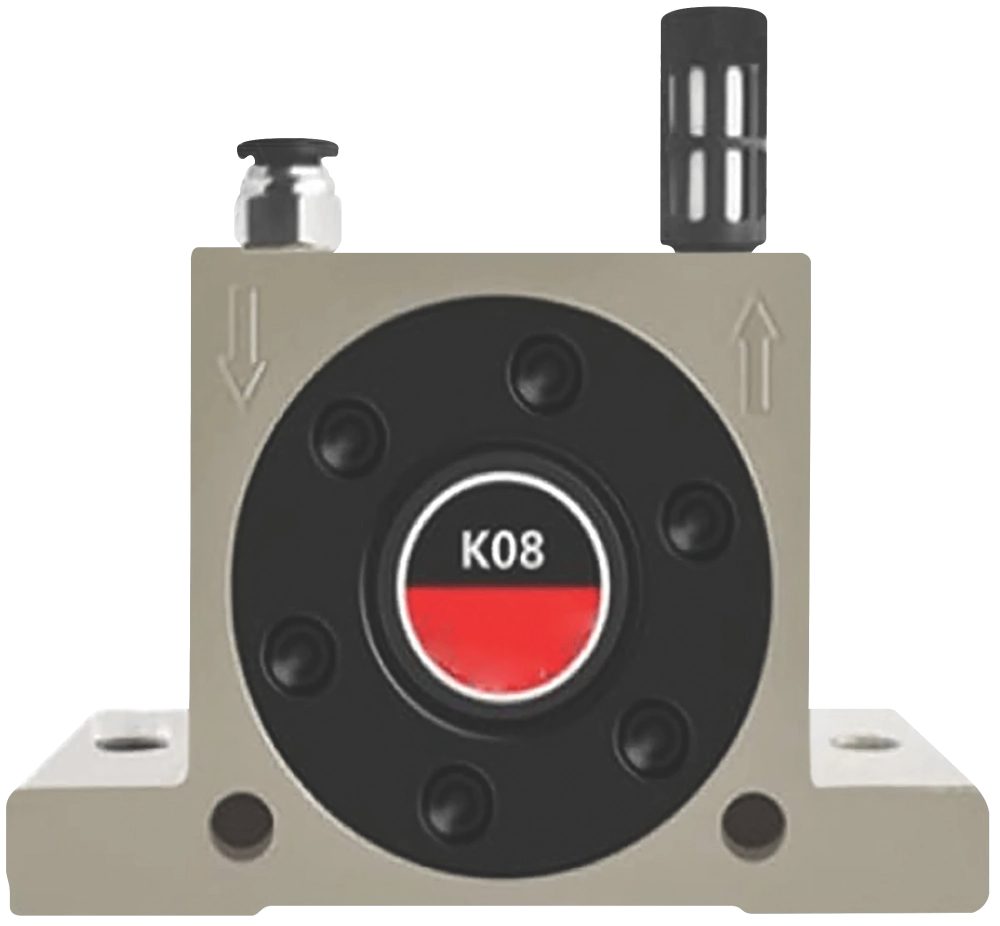
Ball-type air-driven, automation-controlled flow-fluidising unit
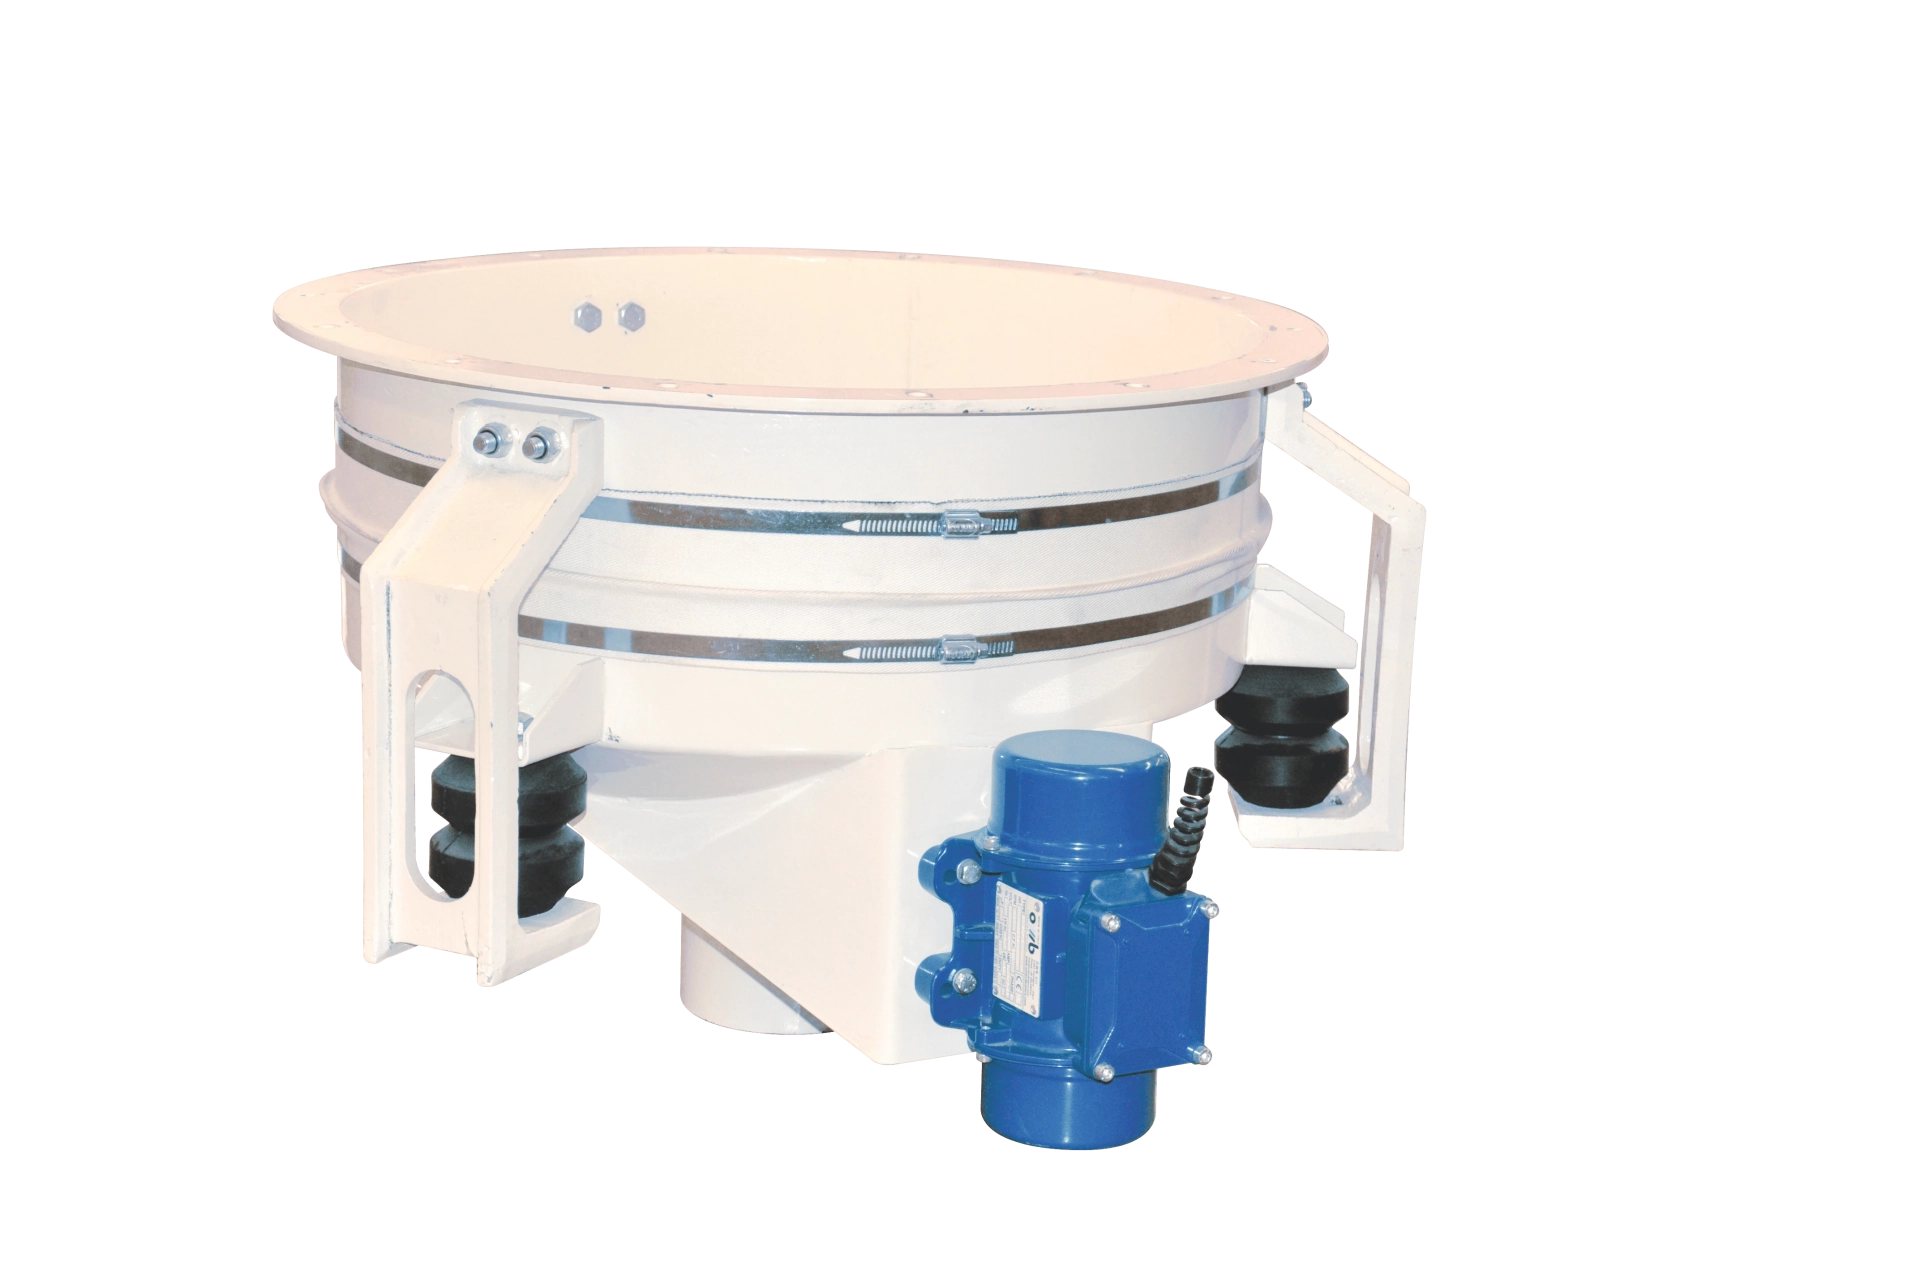
A high-frequency mechanical knocking unit for eliminating product build-ups, sticking and chronic blockages on the inner walls of dust and flour hoppers, raw-material silos, cyclones and the collection cones of bag filters. Owing to ball-type pneumatic-vibration technology, it breaks the static resistance of bulk materials and keeps the line flow uninterrupted and stable.
WORKING PRINCIPLE
Integrated solenoid valve and relay management — timer-controlled signal: the smart time relay designed with the system is precisely calibrated within 0.1–30 seconds to the plant’s product-flow intensity; when the set period arrives, an electro-signal triggers the solenoid valve. Ball-type pneumatic-vibration kinematics — high-frequency air drive: as the valve opens, the compressed air entering the system spins a special steel ball inside the vibrator body at high speed on a circular orbit; this motion produces a high-frequency circular vibration wave (knocking effect) transmitted to the hopper walls. Inner-wall cleaning and blockage release — fluidisation and flow assurance: mounted on the outer surface of the hopper or filter cone, the device transmits the micro-impact vibration it creates straight to the inner walls; the flour, bran and dust particles stuck to the walls or having formed a bridge loosen, fluidise in the gravity direction, and the blockage is easily cleared.
KEY ADVANTAGES
- Smart 0.1–30 s pulse calibration: The widely adjustable time-relay infrastructure gives the operator freedom to set a flexible knocking frequency to the product’s moisture and flowability, preventing unnecessary air consumption.
- Various types and sizes in the “Conical Shaker” family: For full fit to your plant’s hopper volume, sheet thickness and the scale of the flow problem, various industrial sizes and mechanical capacities are available in the “conical hammer” model family.
- Electricity-free body — explosion safety (ATEX compliance): Because the vibration-producing main body is fully pneumatic (compressed-air driven), the spark risk in dust-explosion-prone flour and dust stores reduces to zero — 100% work safety.
- Minimum maintenance and easy adaptation: The rigid ball design with a minimised number of moving parts gives a low wear index; it adapts easily within seconds to any steel or stainless wall of existing lines.
ENGINEERING NOTE
The Pneumatic Vibrator (Conical Shaker) is a compact engineering solution that dynamically lowers the material’s wall-friction coefficient (internal friction angle) in flour and semolina processes. The solenoid-valve-controlled pneumatic-impact frequency creates a fluidised-bed effect and reliably prevents micro flour particles from clumping in the hopper corners. This continuous wall-cleaning also permanently eliminates sanitation risks such as insect infestation and mould formation.
 TR
 RU
 ES